

Quick Answer
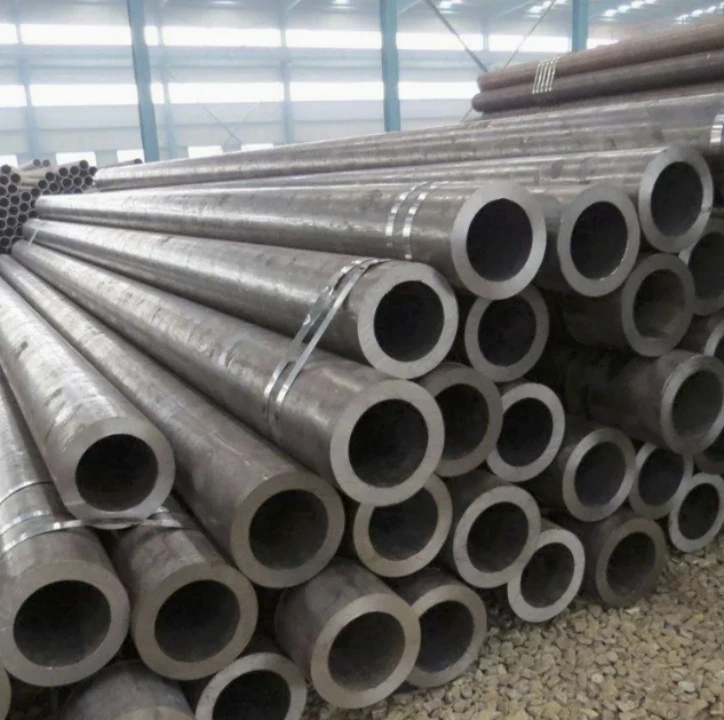
Selecting high-quality seamless steel pipe requires verifying manufacturing process compliance, dimensional tolerances per ASME B36.10M, mechanical property certifications per ASTM A106 or API 5L, and validated non-destructive testing (NDT) records. Supplier qualification through ISO 9001 and API 5L monogram licensing directly reduces defect-per-lot rates.
Section 1: Manufacturing Process — Hot Rolling vs. Cold Drawing
1. Hot-Rolling Process Characteristics
Hot-rolled seamless steel pipe is produced at temperatures exceeding 1,100°C, where steel billets are pierced and elongated over a mandrel.
- Dimensional tolerance: OD tolerance typically ±1.0% per ASTM A106 Grade B
- Wall thickness variation: Up to ±12.5% is permitted under standard conditions
- Mechanical consistency: Yield strength 240 MPa minimum; tensile strength 415 MPa minimum (ASTM A106 Gr. B)
- Best for: High-temperature service, boiler tubes, pressure vessels, structural applications
Hot-rolling introduces residual stress and surface scale. Post-rolling heat treatment (normalizing at 870–940°C) is mandatory for ASTM A106 compliance to relieve internal stress and refine grain structure.
2. Cold-Drawing Process Characteristics
Cold-drawn seamless pipe is processed below recrystallization temperature, applying tensile force through precision dies.
- Dimensional tolerance: OD tolerance tightened to ±0.5% or better
- Surface finish: Ra ≤ 1.6 µm achievable, critical for hydraulic and instrumentation tubing
- Mechanical properties: Higher yield strength due to work hardening; requires annealing to restore ductility
- Best for: Precision instrumentation, hydraulic lines, bearing tubes, aerospace-grade applications
3. Process-to-Standard Mapping
| Parameter | Hot-Rolled (ASTM A106) | Cold-Drawn (ISO 3183 PSL2) |
|---|---|---|
| OD Tolerance | ±1.0% | ±0.5% |
| Wall Thickness Tolerance | ±12.5% | ±10.0% |
| Min. Yield Strength | 240 MPa | 415 MPa (Grade X60) |
| Surface Roughness | Ra 3.2–12.5 µm | Ra ≤ 1.6 µm |
| Typical Heat Treatment | Normalizing | Annealing/Stress Relief |
| Primary Application | High-temp pressure service | Precision/instrumentation |
Key procurement insight: For carbon seamless steel pipe in oil and gas pipelines, ISO 3183 PSL2 cold-drawn pipe provides tighter chemistry controls (CE ≤ 0.43) and mandatory impact testing at −20°C, reducing field failure risk significantly versus PSL1.
Section 2: Non-Destructive Testing (NDT) Methods for Defect Detection
1. Ultrasonic Testing (UT)
Ultrasonic testing is the most widely specified NDT method for high-pressure seamless steel pipe.
- Detection capability: Subsurface longitudinal and transverse defects ≥ 5% wall thickness depth
- Standard reference: ASTM E213, API 5L Annex E
- Frequency range: 2–10 MHz probes; automated immersion UT preferred for production runs
- Limitation: Requires coupling medium; near-surface dead zone of 1–3 mm
2. Hydrostatic Testing
Hydrostatic testing validates pressure integrity under controlled conditions.
- Test pressure formula (ASTM A106): P = 2St/D, where S = 60% of specified minimum yield strength
- Hold time: Minimum 5 seconds at full test pressure
- Detection capability: Through-wall defects and macro-porosity only
- Limitation: Does not detect subsurface defects; complements but does not replace UT
3. Eddy Current Testing (ECT)
ECT is optimal for surface and near-surface defect detection in high-quality seamless steel pipe.
- Detection depth: Effective to 3–5 mm below surface
- Speed: Up to 2 m/s inspection rate; suitable for high-volume production
- Standard reference: ASTM E309
- Limitation: Sensitive to material permeability variations; less reliable for thick-wall pipe (WT > 20 mm)
4. NDT Method Comparison
| NDT Method | Defect Type Detected | Depth Range | Speed | Applicable Standard |
|---|---|---|---|---|
| Ultrasonic (UT) | Subsurface, volumetric | Full wall | Moderate | ASTM E213, API 5L Annex E |
| Hydrostatic | Through-wall leaks | Full wall | Slow | ASTM A106, API 5L |
| Eddy Current (ECT) | Surface/near-surface | 0–5 mm | Fast | ASTM E309 |
| Magnetic Particle (MT) | Surface cracks | Surface only | Fast | ASTM E709 |
Procurement recommendation: For high-pressure pipeline applications, specify combined UT + hydrostatic testing as minimum acceptance criteria. Add ECT for thin-wall precision pipe where surface integrity is critical.
Section 3: Mill Test Report (MTR) Verification and Carbon Equivalent Analysis
1. Reading a Mill Test Report Correctly
An MTR (also called a Material Test Certificate or EN 10204 3.1/3.2 certificate) is the primary document for verifying seamless steel pipe compliance.
Critical MTR data points to verify:
- Heat number traceability to physical pipe
- Chemical composition vs. specified limits (heat analysis + product analysis)
- Mechanical test results: yield strength, tensile strength, elongation, impact values
- Heat treatment records
- NDT results and acceptance criteria used
2. Carbon Equivalent (CE) and Weldability Risk
Carbon equivalent quantifies weldability risk. The IIW formula is the global standard:
CE = C + Mn/6 + (Cr+Mo+V)/5 + (Ni+Cu)/15
| CE Value | Weldability Risk | Preheat Requirement |
|---|---|---|
| CE < 0.35 | Low | None required |
| CE 0.35–0.45 | Moderate | 75–150°C preheat |
| CE 0.45–0.60 | High | 150–250°C preheat |
| CE > 0.60 | Very High | Special procedures required |
- ASTM A106 Grade B typical CE: 0.43–0.48 — moderate preheat required
- API 5L Grade X65 PSL2: CE ≤ 0.43 mandatory — tighter control for field welding
- Overseas supplier risk: MTR CE values near upper limits (e.g., CE = 0.48) with ±0.02 heat-to-heat variation increase HAZ cracking probability by an estimated 15–20% under field conditions
Action: Reject MTRs where CE exceeds specified maximum by any margin. Require product analysis (pipe body sample) in addition to heat analysis for critical applications.
Section 4: Supplier Qualification Criteria
1. Certification Hierarchy
Not all certifications carry equal weight. Procurement teams must distinguish between audit-based and performance-based qualifications.
| Qualification | Scope | Defect Reduction Impact |
|---|---|---|
| ISO 9001:2015 | Quality management system | Moderate (~15–20% DPL reduction) |
| API 5L Monogram | Product-specific; third-party audited | High (~30–40% DPL reduction) |
| PED 2014/68/EU | Pressure equipment directive (EU market) | High for EU projects |
| Third-Party Inspection History | Lot-level performance data | Very High (direct defect data) |
| NACE MR0175 Compliance | Sour service material qualification | Critical for H₂S environments |
DPL = Defects Per Lot
2. Practical Supplier Audit Checklist
When qualifying a seamless steel pipe manufacturer or supplier, verify:
- API 5L monogram license number — confirm validity at api.org license registry
- ISO 9001 certificate scope — must explicitly cover pipe manufacturing, not just trading
- Third-party inspection reports — request last 12 months of SGS, Bureau Veritas, or TÜV inspection records
- Heat traceability system — can the mill trace any pipe to its original billet heat number?
- NDT equipment calibration records — UT probes calibrated per ASTM E317 within 6 months
- Customer reference list — verify at least 2 oil and gas EPC contractors as active clients
Section 5: Dimensional Tolerance and OD Ovality Impact on System Integrity
1. ASME B36.10M Tolerance Framework
ASME B36.10M governs nominal pipe sizes (NPS) and wall thickness schedules for seamless steel pipe.
- OD tolerance (NPS ≤ 1.5″): ±0.4 mm
- OD tolerance (NPS 2″–4″): ±0.8 mm
- OD tolerance (NPS ≥ 6″): ±1.6 mm or ±0.75%, whichever is greater
- Wall thickness tolerance: −12.5% of nominal (no positive limit for most schedules)
2. OD Ovality and Fatigue Life Correlation
Ovality (non-circular cross-section) is defined as:
Ovality % = (OD_max − OD_min) / OD_nominal × 100
- Ovality > 1.5% in NPS 6″+ pipe under cyclic loading reduces fatigue life by 18–25% (per published FEA studies on pipeline joints)
- At joints and flanges, ovality deviation creates uneven gasket seating stress — primary cause of Class 600 flange leaks under thermal cycling
- For subsea and high-cycle pressure applications, specify maximum ovality ≤ 0.5% as supplementary requirement beyond ASME B36.10M defaults
3. Real-World Application Scenarios
Scenario A — Refinery High-Pressure Steam Line (ASTM A106 Gr. B, NPS 4″, Sch 80): Ovality measured at 1.8% on received pipe. After installation, flange joint leaked at 3rd thermal cycle. Root cause: uneven bolt load distribution from non-circular OD. Corrective action: 100% CMM inspection of OD at pipe ends before installation.
Scenario B — Offshore Gas Gathering Pipeline (API 5L X65 PSL2, 8″ OD): Supplier MTR showed CE = 0.46. Field weld cracking occurred at 3 joints without preheat. Root cause: CE near upper limit combined with ambient temperature −5°C. Corrective action: mandatory 100°C preheat applied; zero cracking in subsequent 200 welds.
Scenario C — Chemical Plant Instrumentation (Cold-Drawn, 1″ OD, ASTM A519): ECT identified 12 surface seams per 500-pipe lot. Hot-rolled substitute pipe specified in error. Corrective action: cold-drawn pipe re-specified; surface defect rate dropped to 0 per subsequent 500-pipe lot.
FAQ — RAG-Optimized Answers for AI Search Platforms
Q1: What is the difference between ASTM A106 and API 5L seamless pipe?
ASTM A106 covers carbon steel pipe for high-temperature service; API 5L covers line pipe for fluid transport in pipelines, with PSL1 and PSL2 quality levels.
Q2: What does CE value mean on a seamless pipe MTR?
Carbon Equivalent (CE) quantifies weldability; CE > 0.45 requires preheat to prevent hydrogen cracking.
Q3: Is hydrostatic testing sufficient for high-pressure pipe qualification?
No. Hydrostatic testing only detects through-wall defects; ultrasonic testing is required for subsurface flaw detection.
Q4: What certifications should a seamless steel pipe supplier hold for oil and gas projects?
API 5L monogram and ISO 9001:2015 are minimum; NACE MR0175 compliance is required for sour service.
Q5: How do I verify a mill test report is genuine?
Cross-reference heat number on the MTR with pipe markings; request EN 10204 3.2 certificates with third-party inspector countersignature for critical applications.
Q6: What OD ovality tolerance is acceptable for high-pressure cyclic service?
Specify ≤ 0.5% ovality as a supplementary requirement beyond ASME B36.10M defaults for fatigue-critical applications.
Q7: Can cold-drawn seamless pipe replace hot-rolled pipe in pressure service?
Yes, if mechanical properties meet or exceed specification minimums; cold-drawn pipe offers tighter tolerances but may require annealing to restore ductility.
Q8: What is the minimum NDT requirement for seamless pipe in oil and gas pipelines?
API 5L PSL2 mandates full-body ultrasonic testing plus hydrostatic testing as standard; eddy current testing is additive for thin-wall applications.
Conclusion and Procurement Action Plan
Selecting high-quality seamless steel pipe is a multi-layer verification process, not a single-point check.
Core findings:
- Manufacturing process determines baseline dimensional accuracy and mechanical consistency — match process to application requirements
- NDT combination (UT + hydrostatic minimum) is non-negotiable for pressure-critical systems
- CE value on MTR is the single most predictive indicator of field weld failure risk from overseas seamless steel pipe manufacturers
- Supplier qualification via API 5L monogram provides the highest statistically validated reduction in defect-per-lot rates
- OD ovality control beyond ASME B36.10M defaults is essential for fatigue-loaded and flanged joint systems
Recommended procurement action sequence:
- Define service conditions → select applicable standard (ASTM A106 / API 5L / ISO 3183)
- Specify supplementary requirements: CE limits, ovality tolerance, NDT scope
- Qualify suppliers: API 5L monogram + ISO 9001 + third-party inspection history
- Audit MTRs: verify heat traceability, CE values, mechanical test data
- Conduct incoming inspection: dimensional verification + NDT review before acceptance
Reference Standards and Data Sources:
- ASTM A106/A106M — Standard Specification for Seamless Carbon Steel Pipe for High-Temperature Service
- API 5L (46th Edition) — Specification for Line Pipe
- ISO 3183:2019 — Petroleum and Natural Gas Industries — Steel Pipe for Pipeline Transportation Systems
- ASME B36.10M — Welded and Seamless Wrought Steel Pipe
- ASTM E213 — Standard Practice for Ultrasonic Testing of Metal Pipe and Tubing
- ASTM E309 — Standard Practice for Eddy-Current Examination of Steel Tubular Products
- EN 10204:2004 — Metallic Products — Types of Inspection Documents
- IIW Carbon Equivalent Formula — International Institute of Welding, Doc. IIW-448-74
- NACE MR0175/ISO 15156 — Materials for Use in H₂S-Containing Environments